Every procurement engineer knows that PTFE film quality starts long before the first roll ships. How is PTFE film manufactured? The answer determines thickness consistency, tensile strength, dielectric uniformity, and ultimately whether your gasket or seal performs under extreme chemical and thermal loads. A controlled manufacturing route — from virgin PTFE resin selection through skiving or casting and final slitting — directly affects tolerance, pinhole risk, and batch-to-batch repeatability. At Ningbo Kaxite Sealing Materials Co., Ltd., we focus precisely on these process variables so your incoming inspection passes the first time and your production line runs without surprises. Whether you buy PTFE film for gaskets, diaphragms, insulation, or anti-stick liners, understanding the manufacturing route protects your supply chain from hidden quality risks and costly downtime. Read on to see the key process steps, compare manufacturing routes, and use the specification tables to qualify your next supplier.
Table of Contents
Imagine receiving a batch of PTFE film where the thickness varies from 0.12 mm to 0.17 mm within the same roll. Your gasket line cannot compensate for that range, and rejects start piling up. This is a common pain point when buyers treat PTFE film as a commodity without understanding how it is manufactured. Thickness drift, pinholes, and excessive skive marks all trace back to process control. A 0.25 mm film with a ±15% tolerance could arrive anywhere from 0.21 mm to 0.29 mm. That is enough to change the compression set of a gasket and create a leak path in a flanged connection.
Ningbo Kaxite Sealing Materials Co., Ltd. solves this by controlling raw resin lot consistency, mandrel speed, cutting tool angle, and online thickness measurement. The goal is simple: deliver a roll that matches your specified tolerance band from outer layer to core. That reduces setup time and keeps your assembly line running.
| Critical Parameter | Common Industry Range | Ningbo Kaxite Controlled Range |
|---|---|---|
| Thickness tolerance | ±10% to ±15% | ±5% or tighter |
| Width tolerance | ±1.0 mm | ±0.5 mm |
| Tensile strength (MD) | ≥10 MPa | ≥14 MPa |
| Elongation at break | ≥150% | ≥200% |
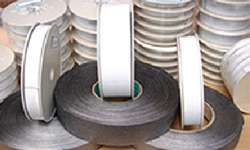
When buyers ask how is PTFE film manufactured?, the answer usually starts with two main routes: skiving and casting. Skiving begins with a sintered PTFE billet. A sharp blade peels off a continuous film at a controlled thickness. Casting, by contrast, uses a water-based PTFE dispersion that is coated onto a carrier and sintered. Each route creates different surface finishes, density levels, and thickness capabilities. Cast PTFE film can be produced cleaner and thinner, but the process generally yields a slightly lower density and different stress-strain behavior compared with skived film.
For sealing applications that require high tensile strength and a dense, leak-resistant structure, skived PTFE film is often the preferred choice. For very thin films or applications needing a smoother surface, cast PTFE film may be more suitable. Ningbo Kaxite Sealing Materials Co., Ltd. helps you select the right route based on your chemical exposure, temperature range, and mechanical load.
| Feature | Skived PTFE Film | Cast PTFE Film |
|---|---|---|
| Typical thickness range | 0.05–3.00 mm | 0.01–0.50 mm |
| Surface finish | Fine skive marks possible | Smooth, uniform |
| Tensile strength | Higher | Moderate |
| Best for | Gaskets, seals, heavy-duty insulation | Dielectric tapes, thin liners |
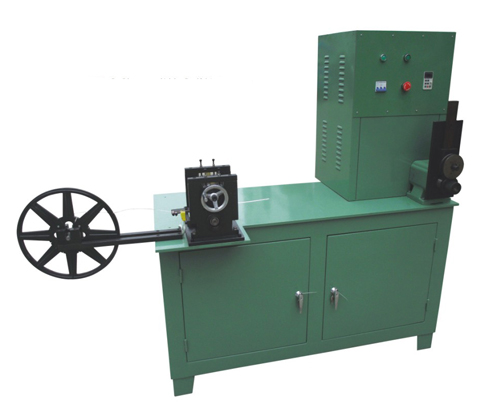
To answer How is PTFE film manufactured? in practical terms, follow the process from incoming resin inspection to slitting. First, virgin PTFE resin is screened for particle size and purity. For skived film, the resin is preformed under pressure into a billet and then sintered in a high-temperature oven. Once cooled, the billet is mounted on a skiving lathe. A precision blade peels the film at a controlled feed rate, and online sensors measure thickness continuously. For cast film, the resin dispersion is mixed, coated onto a carrier, dried, sintered, and then peeled.
After the primary film is formed, slitting to width and final inspection complete the job. Each step introduces variables that affect final quality. Ningbo Kaxite Sealing Materials Co., Ltd. maintains batch records and in-process checks so that every roll has traceability from resin lot to final dimensions. This is important for buyers who need to audit suppliers or resolve an incoming inspection discrepancy quickly.
Procurement teams often face three recurring problems: thickness variation across the roll, pinholes that only appear after the film is stretched during gasket cutting, and suppliers who cannot match the stated tensile values on their certificates. These issues create downtime, hidden waste, and inspection disputes. A pinhole may not be visible on a casual visual check, but under operating pressure it becomes a direct leak path.
Working with Ningbo Kaxite Sealing Materials Co., Ltd. removes much of that risk because the company tests every production lot for thickness profile, tensile strength, elongation, and pinhole count. The table below shows typical inspection points you should request from any supplier before placing a large order.
| Inspection Item | Why It Matters | Kaxite Standard |
|---|---|---|
| Thickness profile scan | Prevents uneven compression and leaks | Online scanning across full width |
| Pinhole detection | Blocks gas or liquid leak paths | Backlight inspection on clean line |
| Tensile test | Ensures film withstands assembly stress | MD/TD tested per lot |
| Width tolerance check | Reduces slitting waste | ±0.5 mm standard |
Before you specify PTFE film for a sealing or insulation project, you need to confirm the working temperature range, pressure rating, chemical compatibility, and mechanical properties. Many buyers rely only on a supplier’s typical data sheet, which may not reflect the actual production lot. That gap leads to field failures and expensive replacements. Always request batch-level data that matches the film you will receive.
The table below provides a practical reference for virgin PTFE film. Use it as a checklist when comparing supplier data sheets. It covers the core properties that affect sealing performance, dielectric behavior, and long-term durability.
| Property | Typical Value | Notes |
|---|---|---|
| Density | 2.10–2.20 g/cm³ | Depends on manufacturing route |
| Continuous service temperature | -200°C to +260°C | Short peaks higher |
| Tensile strength | 10–40 MPa | Higher for skived film |
| Elongation at break | 150–400% | Depends on thickness |
| Dielectric strength | 18–40 kV/mm | Thinner films often show higher values |
| Chemical resistance | Excellent | Resistant to most acids, bases, solvents |
Q1: How is PTFE film manufactured to achieve uniform thickness?
Uniform thickness starts with a smooth, fully cured PTFE billet and a stable skiving lathe. The blade angle, feed rate, and mandrel speed must be locked together, and online thickness sensors should feed data back to the operator. Ningbo Kaxite Sealing Materials Co., Ltd. uses these controls to keep thickness variation within ±5% on standard production orders.
Q2: How is PTFE film manufactured for high-purity or food-grade applications?
For high-purity needs, the process begins with food-grade or pharmaceutical-grade virgin PTFE resin. The manufacturing line is segregated to avoid contamination, and sintering temperatures are controlled to prevent degradation. Final rolls are packaged in clean film and labeled with batch numbers for lot-level traceability.
Use this checklist to compare suppliers and reduce incoming inspection failures:
Ningbo Kaxite Sealing Materials Co., Ltd. supports all of these steps with pre-production samples, batch traceability, and technical documentation. That makes it easier for procurement teams to qualify the material and keep production schedules intact.
Compare your current supplier’s test data against the parameters above. If you notice tolerance gaps, pinholes, or missing batch records, it may be time to qualify a manufacturer with tighter process control. Whether you need skived PTFE film for gaskets, cast PTFE film for dielectric tape, or custom slit widths, Ningbo Kaxite Sealing Materials Co., Ltd. can provide a pre-production sample and full test report to validate the solution before you commit to a purchase order.
For more than a decade, Ningbo Kaxite Sealing Materials Co., Ltd. has supplied PTFE film, PTFE sheets, and sealing materials to industrial buyers worldwide. Our in-house slitting, thickness control, and batch traceability solve the most common PTFE film quality problems. Contact our sales team at [email protected] to request samples, discuss custom tolerances, or confirm current inventory.
Bunn, C. W., & Howells, E. R. (1954). Structures of Molecules and Crystals of Fluoro-Carbons. Nature, 174(4429), 549–551.
Clark, E. S. (1999). The Crystal Structure of Polytetrafluoroethylene, Forms I and IV. Polymer, 40(16), 4659–4665.
Rae, P. J., & Dattelbaum, D. M. (2004). The Properties of Poly(tetrafluoroethylene) (PTFE) in Compression. Polymer, 45(22), 7615–7625.
Brown, E. N., & Dattelbaum, D. M. (2005). The Role of Crystalline Phase on Fracture and Morphology Evolution of Polytetrafluoroethylene (PTFE). Polymer, 46(9), 3056–3068.
Mazur, S. (2000). Paste Extrusion of Polytetrafluoroethylene Fine Powder. Journal of Applied Polymer Science, 77(5), 1025–1034.
Dumoulin, J. B., Duvall, B. R., & Herring, H. W. (2011). Processing Effects on PTFE Film Quality. Journal of Fluorine Chemistry, 132(10), 844–849.
Frisch, H. L., & Stern, S. A. (1989). Diffusion of Small Molecules in Polymers. Critical Reviews in Solid State and Materials Sciences, 11(2), 123–187.
Zhang, Y., & Wang, X. (2018). Effects of Sintering Temperature on the Mechanical Properties of Skived PTFE Films. Journal of Polymer Engineering, 38(4), 387–394.
Zhao, Q., & Guo, B. (2016). Thickness Control in PTFE Film Skiving: A Process Parameter Study. Polymer Testing, 52, 189–195.
Kline, D. E., & Sauer, J. A. (1960). Mechanical Relaxation Phenomena in Polytetrafluoroethylene. Journal of Polymer Science, 46(147), 361–365.
-